How Brazing Turns Plates & Bars Into a High-Performance Heat Exchanger
Posted on September 16, 2026
No bolts. No gaskets. No weak points. Just metal fused into metal — here’s the science behind one of industrial manufacturing’s most underrated processes.
Walk into any serious industrial facility — gas processing plant, petrochemical unit, cryogenic separation line — and somewhere in that maze of pipework sits a component doing enormous, invisible work: the Heat Exchanger. It moves thermal energy from one fluid stream to another without ever letting them touch, hour after hour, at pressures and temperatures that would destroy a lesser-built unit.
What makes a plate-and-bar heat exchanger tough enough for that job isn’t the aluminum itself. It’s how the aluminum is joined. And that answer, almost every time, is brazing.
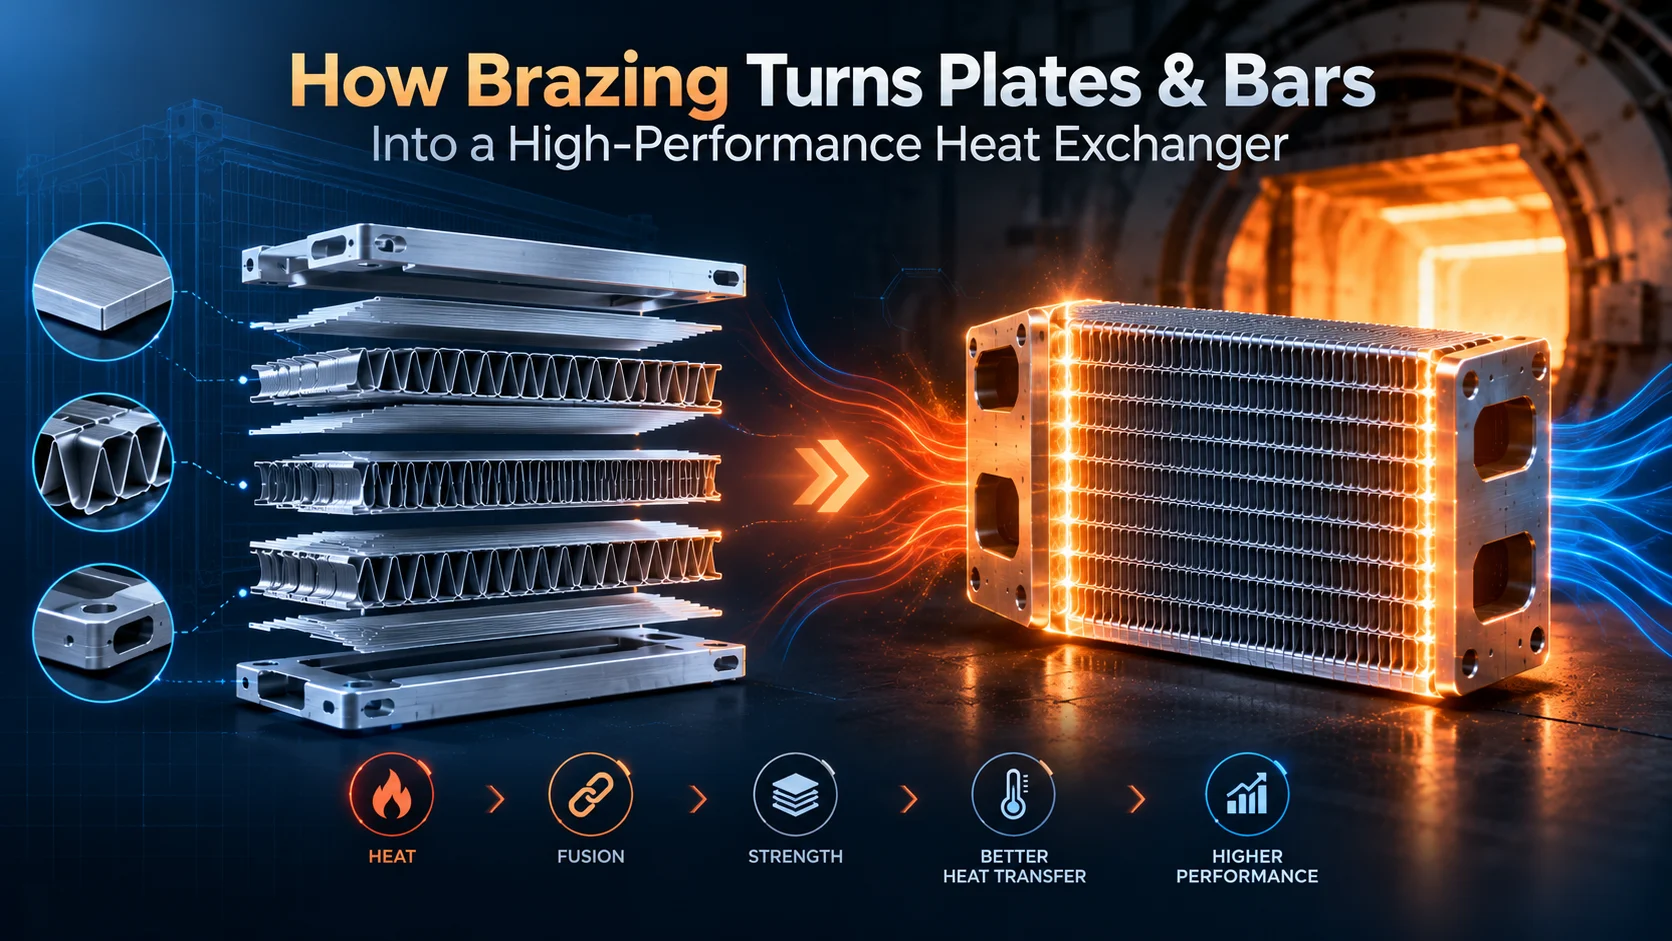
This is the process that takes a loose stack of plates, corrugated fins, and side bars — components that, on their own, couldn’t hold back a bucket of water — and fuses them into a single, monolithic, leak-proof core. Let’s break down exactly how it works, and why it matters so much for anyone specifying industrial heat transfer equipment.
First, What Are We Actually Building?
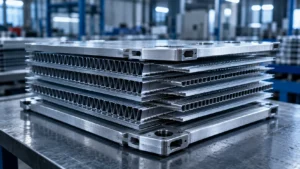
A plate-and-bar (or “bar-plate”) heat exchanger is built from three repeating components, stacked layer upon layer:
- Parting plates — thin aluminum sheets that separate one fluid stream from the next
- Corrugated fins — folded aluminum inserts sandwiched between plates that dramatically increase surface area for heat transfer
- Side bars — solid aluminum strips that seal the edges of each layer, containing the fluid within its channel
Stack enough of these in alternating layers — hot stream, cold stream, hot stream, cold stream — and you get a compact core capable of transferring enormous amounts of heat in a fraction of the footprint of a shell-and-tube unit. But right now, it’s just a pile of parts. Brazing is what turns it into a machine.
The Brazing Process, Step by Step
- Cladding — the “glue” is already built in Before assembly even starts, plates are clad with a thin layer of aluminum-silicon brazing alloy — a filler metal engineered to melt at a lower temperature than the structural aluminum around it. This is the detail most people miss: the bonding material isn’t added later. It’s rolled directly onto the plate surface from the start.
- Stacking — precision by design Plates, fins, and bars are layered in exact sequence to form the internal flow channels for each fluid stream. Every joint, every contact point, has to align perfectly — because there’s no second chance to fix a misaligned stack once it’s in the furnace.
- Loading under pressure The full stack is clamped or weighted to hold every layer in firm contact. Even a fraction of a millimeter of gap at this stage can become a leak path later — this is where manufacturing discipline separates a premium Heat exchanger manufacturer in India from a shortcut-taking one.
- Furnace brazing — vacuum or inert atmosphere The stack goes into a furnace and is heated to the point where the cladding layer melts — but not the structural plates themselves. Critically, this happens under vacuum or an inert gas atmosphere (typically nitrogen). Why? Aluminum oxidizes almost instantly in open air, and that oxide skin blocks the filler metal from properly wetting and bonding the joint. Skip this step, or do it poorly, and you get a core that looks fine but fails under pressure.
- Capillary flow — the molten metal does the work As the filler melts, it’s drawn into every microscopic gap between plates, fins, and bars by capillary action — flowing exactly where it’s needed, sealing every contact point simultaneously across the entire core.
- Controlled cooling — one shot, one solid core As the furnace cools, the molten filler solidifies everywhere at once. Plates, fins, and bars become a single rigid structure — not fastened together, but genuinely fused, atom-bonded at every joint.
Why This Process Actually Matters
| Mechanically Assembled (Gasketed) | Brazed Plate-and-Bar |
| Gaskets age, harden, and leak over time | No gaskets — nothing to degrade |
| Bolted joints can loosen under vibration | Fused joints, no moving fasteners |
| Limited pressure/temperature ratings | Handles extreme pressure and thermal cycling |
| Bulkier for the same duty | Highly compact, lightweight core |
| Easier to service, but more failure points | Fewer failure points, longer service life |
For industries running continuous, high-stakes thermal processes — gas separation, LNG, refining, industrial refrigeration — that compactness and reliability isn’t a nice-to-have. It’s the difference between planned maintenance and unplanned downtime.
Where Brazing Quality Actually Gets Tested
Because the entire core is joined in a single furnace cycle, there’s zero room for error. A few degrees of temperature drift, uneven clamping pressure, or trace contamination on a plate surface can leave a micro-gap invisible to the eye — one that only reveals itself as a leak months later, under real operating pressure.
This is exactly why brazing quality isn’t something you take on faith. It’s verified through:
- Dye-penetrant testing to catch surface-level joint defects
- Helium leak testing to confirm the core holds pressure under real-world conditions
- X-ray or ultrasonic inspection for internal joint integrity where the process demands zero tolerance for failure
A manufacturer that treats these checks as standard practice — not an optional add-on — is the difference between a heat exchanger that performs for one thermal cycle and one that performs for a decade of them.
Choosing a Manufacturer That Gets This Right
Not every Plate & Bar manufacturer in India runs vacuum-brazing to the same standard. Furnace atmosphere control, clamping precision, alloy selection, and post-braze inspection are all places where corners can quietly get cut — and where the cost of a shortcut only shows up after the unit is already in the field, under pressure, with no easy way to inspect it from the outside.
This is where NBR Cooling Systems approaches things differently — treating brazing not as one manufacturing step among many, but as the step that determines whether a heat exchanger lasts one thermal cycle or ten thousand. As a Heat exchanger manufacturer in India built around precision-engineered plate-and-bar cores, the focus stays on getting the fundamentals — cladding, atmosphere control, capillary flow, and post-braze verification — right every single time, not just on paper.
The Bottom Line: It All Comes Down to One Furnace Cycle
Brazing isn’t a finishing touch on a plate-and-bar heat exchanger — it is the heat exchanger. Every plate, fin, and bar is only as good as the joint holding it to its neighbor, and that joint is only as good as the furnace process that created it. Understanding this process isn’t just useful for engineers on the manufacturing floor — it’s exactly what anyone specifying or procuring industrial heat transfer equipment should be asking their supplier about before signing off on a purchase order.
FAQs
Can a brazed plate-and-bar heat exchanger be repaired if it leaks?
Rarely. Since the entire core is brazed in one furnace cycle, reheating one joint can affect surrounding joints. Specialist repairs exist for isolated leaks, but replacement is generally more reliable.
What’s the difference between brazing and welding a heat exchanger?
Welding melts the base metal, while brazing melts only the filler metal. This makes brazing ideal for joining thin plates and complex geometries without significantly warping the base material.
How long does a well-brazed heat exchanger last? With clean fluids, proper operating conditions, and quality manufacturing, plate-and-bar heat exchangers can commonly last 10–20+ years. Brazing quality, alloy selection, and furnace control are key factors.
Why do brazed heat exchangers develop leaks?
Leaks can result from poor clamping, oxidation, uneven braze alloy distribution, fouling, or corrosive fluids. Manufacturing quality is particularly important in preventing premature failures.
Is a brazed heat exchanger better than a gasketed plate-and-frame exchanger?
It depends on the application. Brazed units are compact and eliminate gasket maintenance, while gasketed units can be opened for mechanical cleaning. Brazed designs suit clean fluids and demanding pressure or temperature conditions.
Can you weld-repair a leaking brazed aluminum heat exchanger?
Technically, yes, but results can be inconsistent. Previous brazing can affect the base metal and make welding less reliable, so it is generally considered a temporary solution rather than a long-term repair.
What material is used as brazing filler, and does it matter?
Aluminum plate-and-bar cores typically use aluminum-silicon alloys, while stainless-steel units commonly use copper- or nickel-based fillers. The choice affects melting temperature, corrosion resistance, and fluid compatibility.